
Description
Belt Conveyor System – Product Description
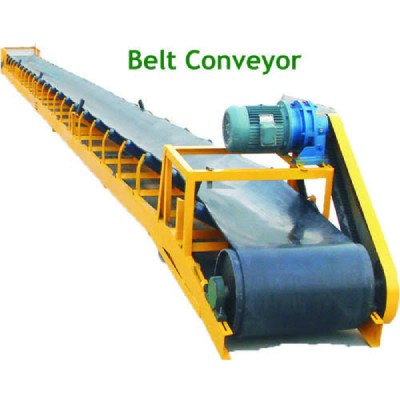
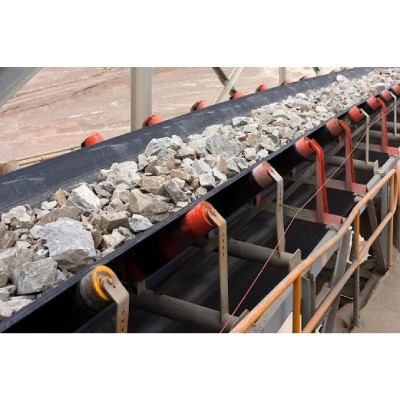
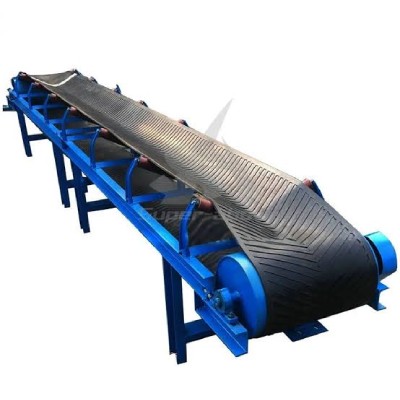
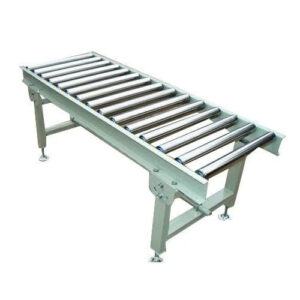
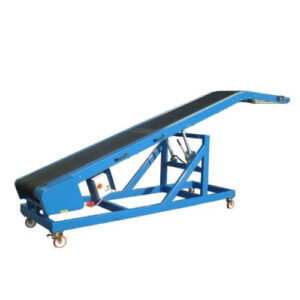
A Belt Conveyor System is a continuous material handling solution designed to efficiently transport bulk materials or unit loads across various distances, inclinations, and processing stages. Utilizing a belt looped over pulleys and supported by idler rollers, this system ensures smooth, safe, and cost-effective transportation of materials in industries such as mining, cement, power, agriculture, and manufacturing.
Key Features:
-
Modular & Scalable Design: Available in fixed, portable, or extendable configurations to suit any layout or load requirement.
-
High Efficiency: Capable of moving large volumes of material with minimal energy consumption.
-
Versatile Handling: Supports light to heavy-duty applications with options for flat, inclined, or troughed conveying.
-
Durable Construction: Built with high-quality steel frames, heavy-duty pulleys, and wear-resistant belts.
-
Low Maintenance: Sealed bearings, self-cleaning components, and modular parts reduce downtime and operational cost.
-
Safety Integrated: Includes guards, emergency stop switches, belt alignment sensors, and speed monitors as standard or optional features.
Applications:
-
Mining & Quarrying
-
Cement & Aggregate Plants
-
Power Plants (Coal and Ash Handling)
-
Fertilizer & Chemical Industries
-
Ports, Terminals & Ship Loading
-
Food, Grain, and Packaging Industries
Benefits:
-
Reduces manual handling and increases productivity
-
Low operating cost with high throughput capacity
-
Customizable to site-specific requirements
-
Easy to integrate into existing systems or automation lines
-
Designed for long-term, continuous operation in harsh environments
Let me know if you’d like:
-
A custom version (e.g., mobile conveyor, stacking conveyor, enclosed conveyor)
-
A flow diagram or layout drawing
-
Integration options with weighing, metal detection, or automation systems
-
A costing breakdown or ROI analysis
Reviews
There are no reviews yet.